Food
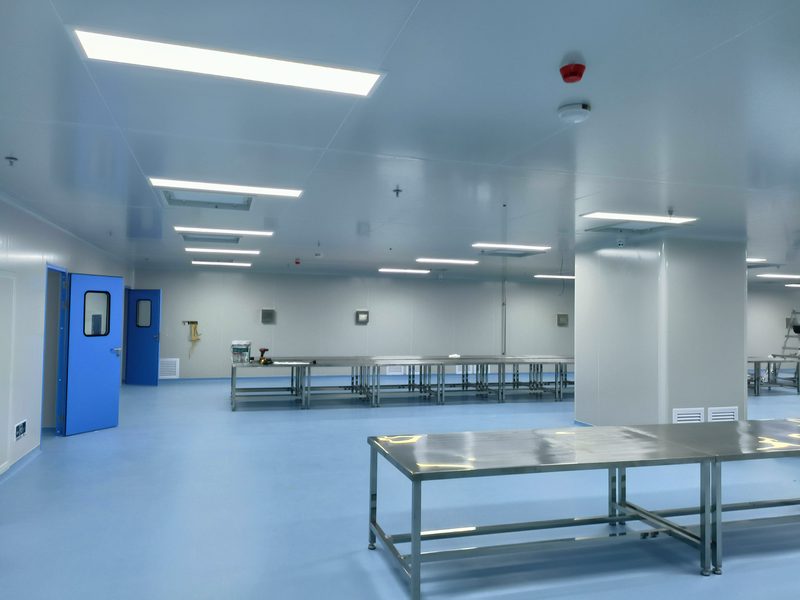
SC-certified workshop
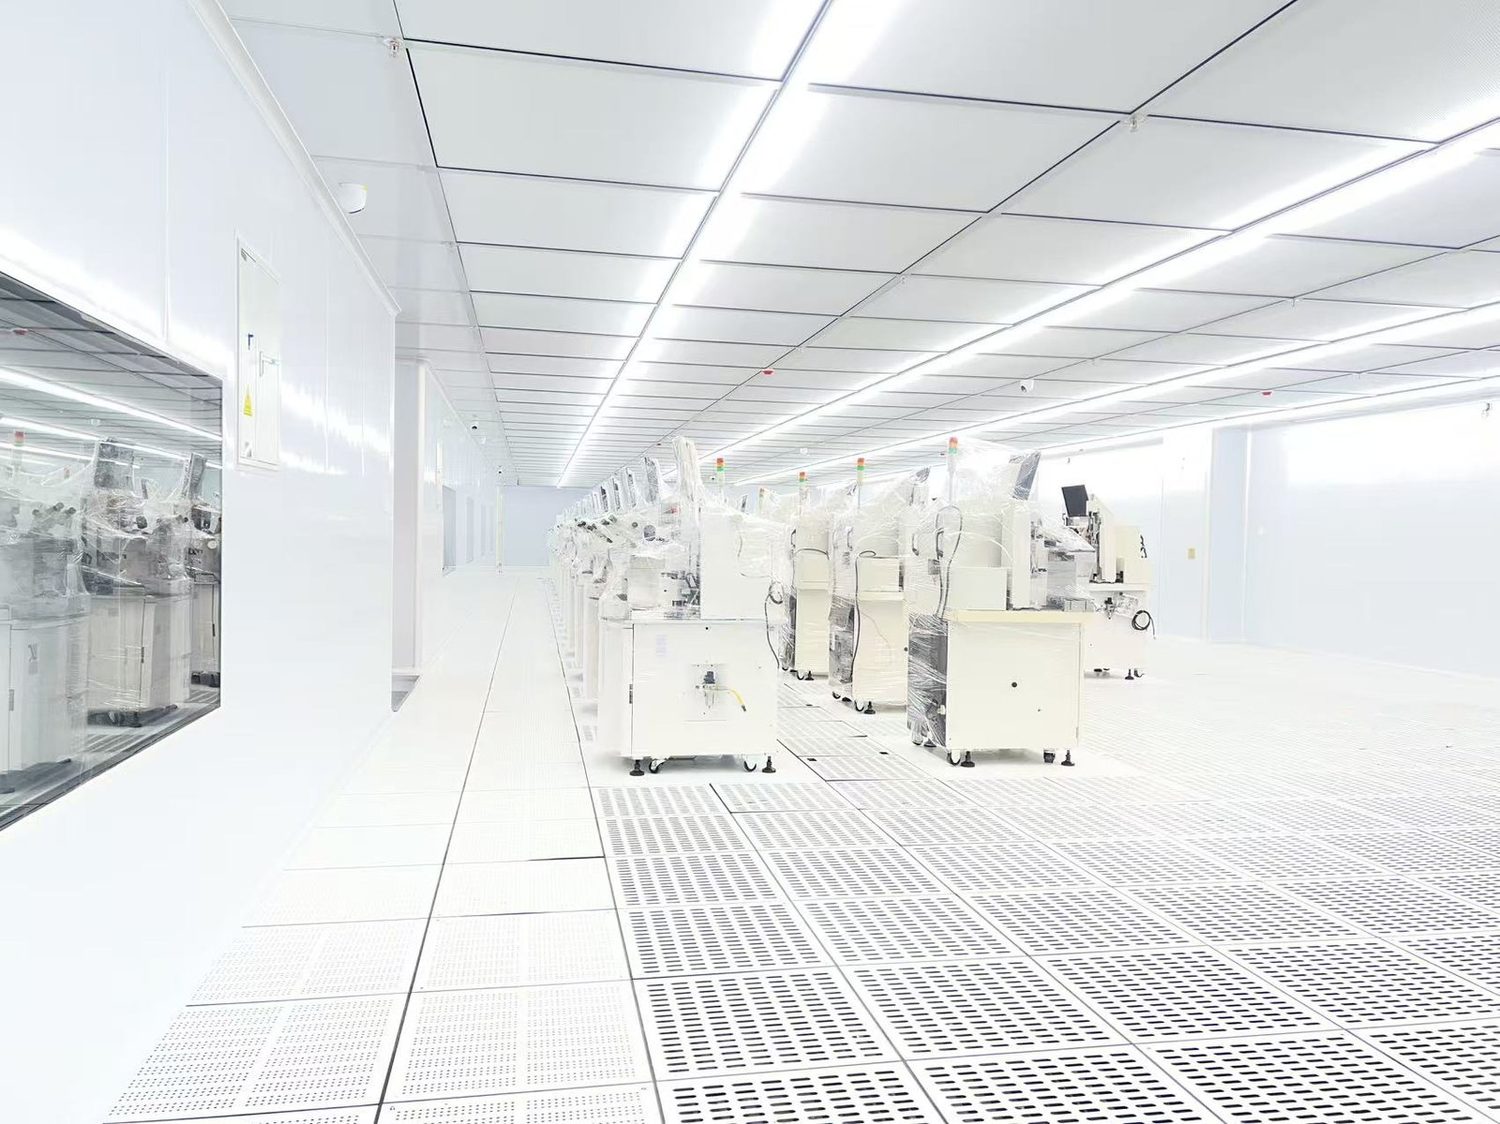
We deliver integrated design, construction and maintenance of cleanrooms and purification systems. Full-range capability from ISO Class 5 to ISO Class 8, with dew point control down to -40℃ — building safe, stable and efficient production and R&D environments for semiconductor, lithium battery, medical device, electronics and food industries.
Guangdong Rongfa Environmental Technology Co., Ltd. specialises in the integrated design, construction and maintenance of cleanrooms and purification systems. We serve the semiconductor, new-energy lithium battery, medical device, electronics and food processing sectors, with full-range engineering capability from ISO Class 5 (Class 100) through ISO Class 8 (Class 100,000).
Our core technical team has deep roots in the cleanroom industry and masters a range of key technologies: ultra-low dew point dry rooms, AMC (airborne molecular contaminant) control, GMP-compliant clean workshops, anti-static systems and precision temperature/humidity control. We have delivered clean-environment solutions for a number of industry leaders.
Guided by the principle of "quality first, technology leadership", we combine rigorous project management with excellent workmanship to build production and R&D environments that are safe, stable and highly efficient.